An AQL number is not a defect tolerance. It is a probability statement about a batch, and most disputes over metal souvenir quality happen because a buyer treats it as something else. Writing “AQL 2.5” on a purchase order without naming the defect classification, the inspection level, the lot definition and the sample size leaves the acceptance decision to whoever picks up the phone last. A buyer who specifies those four things has a dispute mechanism that works, because both sides are working from the same published tables rather than from memory. This guide covers how the sampling system behind those tables actually operates, what the 2026 revision of the international standard changed, and how to write an acceptance clause that a third-party inspector can apply without asking a question.
Custom metal souvenirs are a difficult category to inspect statistically, and that difficulty is the reason the discussion gets emotional. A part is three-dimensional, its defects are distributed across a face rather than a surface, and the defects that matter most to a buyer are often visual and subjective: a plating shade that has drifted, a relief that reads soft, an engraved logo that is slightly off-centre. Each of these is easy to argue about in person and impossible to argue about consistently across three hundred sampled pieces. The sampling tables exist to convert that argument into a number before the container is packed.
What follows assumes no prior knowledge of the system. It sets out the structure first, then the mechanics, then the parts of it that most often cause trouble.
What the standard is and which version applies
The international standard is ISO 2859-1, titled Sampling procedures for inspection by attributes — Part 1: Sampling schemes indexed by acceptance quality limit (AQL) for lot-by-lot inspection. The current edition is ISO 2859-1:2026, published on 22 January 2026 as Edition 3, and it replaces the 1999 edition together with its amendment and corrigendum. The official standard page describes it as the international standard that defines a system of acceptance sampling plans for inspection by attributes, enabling organisations to assess the quality of products or processes based on sample-based inspections, and states that it works best alongside ISO 2859-0 for illustrative examples while providing everything needed to define AQL-indexed single, double or multiple sampling schemes.
The North American equivalent carries a different designation. ANSI/ASQ Z1.4 is the American national version of the same methodology and is described in the inspection literature as technically identical to ISO 2859-1, with the same tables and procedures; the two names are used interchangeably in contracts depending on which document the buyer cites. The historical parent is MIL-STD-105, first published in 1950 and revised through MIL-STD-105E in 1989, which established the Dodge-Romig and Shewhart foundations for attributes sampling; it was superseded and is no longer current.
Three changes in the 2026 edition matter for a buyer writing a contract clause. The edition introduces skip-lot sampling procedures as a formal option, along with the rules for switching from normal or reduced inspection into skip-lot, the qualification conditions for producers and products, and guidance on skip-lot validity including how batches are selected at random. It replaces the printed operating characteristic and average sample number tables with curve generation methods moved into an appendix. And it clarifies the relationship with ISO 2859-2 and ISO 2859-3. The practical consequence for a buyer is that the 2026 edition supports a lighter inspection regime for a consistently good supplier, which is a commercial benefit, but only if the qualification conditions are met and written into the arrangement. The official abstract is available on the ISO catalogue page for ISO 2859-1:2026, and a readable rendering of the scope and clause structure appears in the national adoption listing.
Defect classification: the part buyers skip
Before any table is consulted, every defect has to be assigned to a severity class, because each class carries its own AQL and its own accept and reject numbers. Three classes are conventional. Critical defects are those that pose a safety hazard or violate regulations. Major defects affect function or appearance and are likely to cause a return. Minor defects are slight flaws such as a scratch in a hidden area, minor colour variation or a loose thread.
The most widely used combination in international trade is critical at 0, major at 2.5 and minor at 4.0. The numbers are not the only sensible choice: a medical device manufacturer might run 0 / 1.0 / 2.5, while a promotional goods buyer might accept 0 / 4.0 / 6.5. What is not acceptable is leaving the classification to the inspector, because a defect that one inspector calls minor and another calls major produces a pass and a fail from identical goods. This AQL table guide explains the classification and the level structure in more detail, and it is the reference most useful when briefing an inspection provider that has not seen the product before.
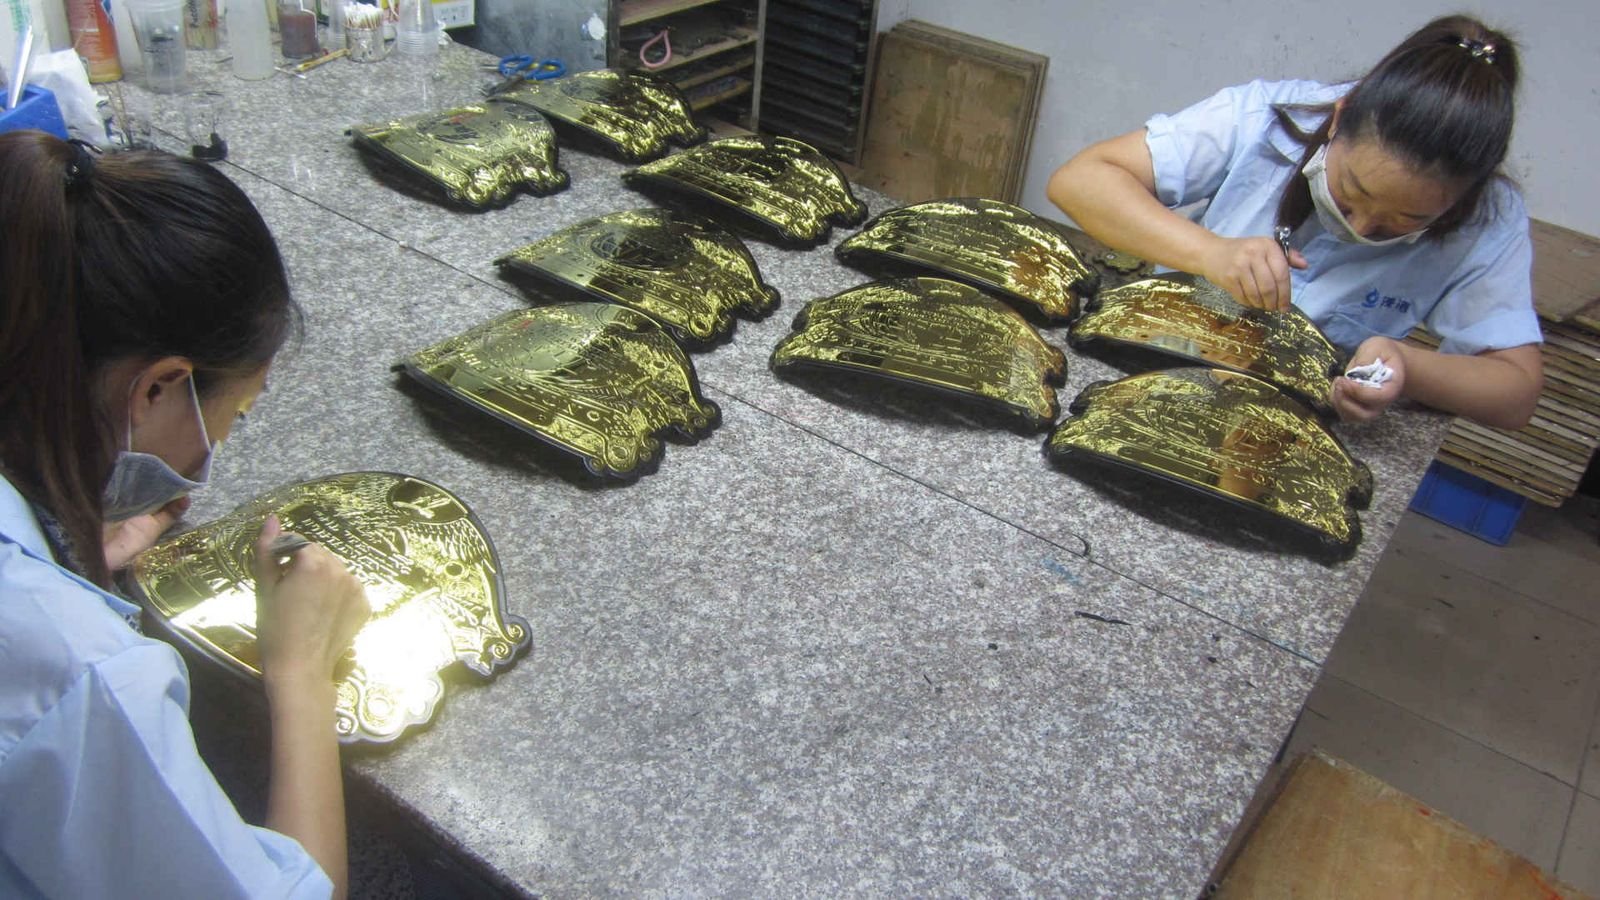
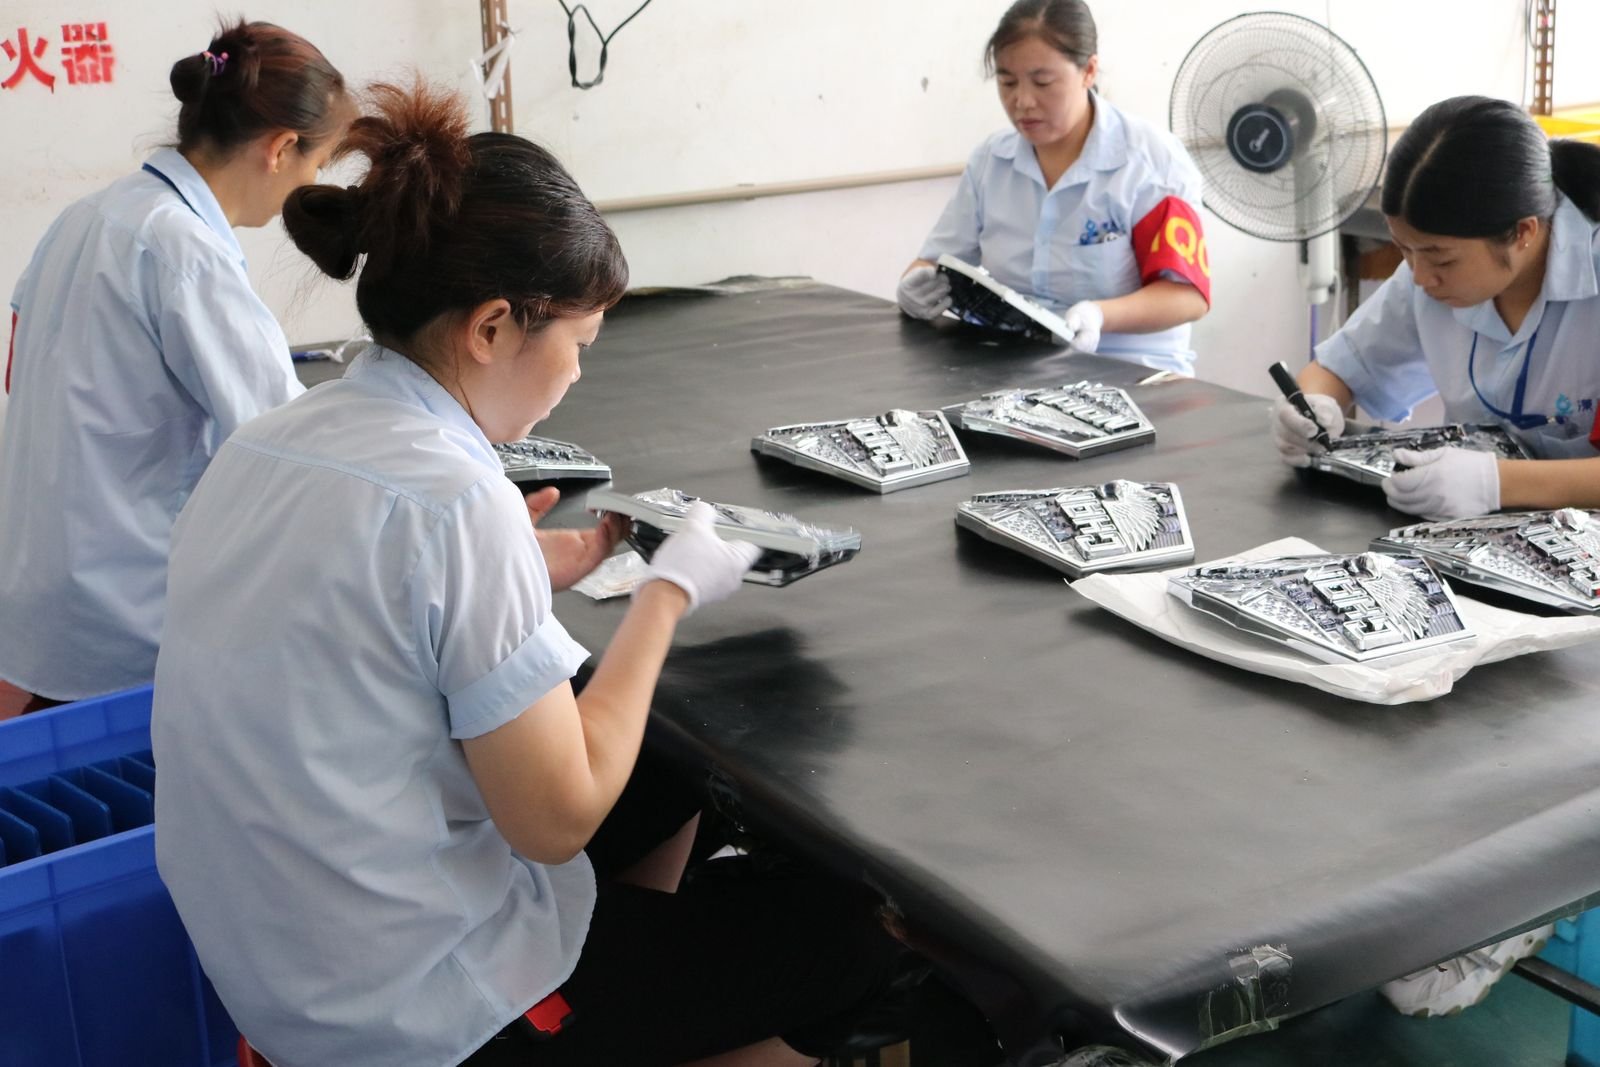
For metal souvenirs specifically, the classification should be written against physical features rather than adjectives, because that is what an inspector can apply to a random piece without a conversation. A workable critical class for this category covers sharp edges that fail to meet the intended handling safety, loose or detachable small parts including chain and ring attachments, and any finish defect on a part designated for direct skin contact. A workable major class covers plating bare spots, visible pits or porosity on a face, a logo that is missing, misaligned or incomplete, dimensions outside the drawing tolerance on a designated feature, and colour outside the agreed reference band. Minor class covers fine scratches on reverse surfaces, light surface marks that do not show at arm’s length, and minor colour variance within an agreed band.
The two-table lookup
Once defects are classified, finding the sample size is a two-step lookup in the tables of the standard. This is the part that most first-time buyers find counter-intuitive, because the lot size does not appear in the second step at all.
Step one uses the lot size and the inspection level together to produce a sample size code letter. Step two takes that code letter and the chosen AQL to produce both the sample size and the acceptance and rejection numbers. The lot size enters the system once and only once.
Table 1 below reproduces the code letter lookup for General Inspection Level II, which is the default used for most consumer goods inspection and the level specified for most metal souvenir orders. The same lot size produces a different code letter under Level I or Level III, because a higher level means a larger sample and greater discrimination.
| Lot size | Code letter (General II) | Sample size |
|---|---|---|
| 2 to 8 | A | 2 |
| 9 to 15 | B | 3 |
| 16 to 25 | C | 5 |
| 26 to 50 | D | 8 |
| 51 to 90 | E | 13 |
| 91 to 150 | F | 20 |
| 151 to 280 | G | 32 |
| 281 to 500 | H | 50 |
| 501 to 1,200 | J | 80 |
| 1,201 to 3,200 | K | 125 |
| 3,201 to 10,000 | L | 200 |
| 10,001 to 35,000 | M | 315 |
| 35,001 to 150,000 | N | 500 |
| 150,001 to 500,000 | P | 800 |
| 500,001 and over | Q | 1,250 |
Two features of this table are worth noting. Sample size grows much more slowly than lot size, because statistical reliability depends on the absolute number of pieces examined rather than on the proportion of the batch inspected: a batch of 500 needs 50 pieces examined, which is a tenth of the lot, while a batch of 35,000 needs 315, which is under 1%. And the sample size steps are large at the bottom of the range, which is why small orders are sometimes inspected at a higher level than the default purely to get a workable number of pieces to look at.
Step two produces the accept and reject numbers. Table 2 shows the single sampling plan for General Inspection Level II at code letter K, sample size 125, which is the plan that covers a lot of 1,201 to 3,200 pieces.
| AQL | Accept (Ac) | Reject (Re) |
|---|---|---|
| 0.065 | 0 | 1 |
| 0.10 | 0 | 1 |
| 0.15 | 1 | 2 |
| 0.25 | 2 | 3 |
| 0.40 | 3 | 4 |
| 0.65 | 5 | 6 |
| 1.0 | 7 | 8 |
| 1.5 | 10 | 11 |
| 2.5 | 14 | 15 |
| 4.0 | 21 | 22 |
The arithmetic of the plan is simple once the numbers are in front of you. A lot of 3,000 pieces inspected at General Level II returns code letter K and a sample of 125 units. At AQL 2.5 for major defects, that lot is accepted on 14 defects and rejected on 15. A lot of 500 at the same level returns code letter H and a sample of 50, accepted on 3 major defects and rejected on 4. A lot of 12,000 returns code letter M and a sample of 315, accepted on 14 and rejected on 15 for the same AQL. This is the same table reproduced across the inspection literature, and the working example from the AQL sampling table reference uses the identical 3,200-unit lot returning code letter K with 125 units sampled, accepted on 7 and rejected on 8 at AQL 2.5.
One point in that worked example deserves emphasis, because it trips people up. The value 7 and 8 belongs to AQL 1.0 for code letter K, not to AQL 2.5, which reads 14 and 15 in the table above. A buyer who copies acceptance numbers from a worked example without checking the AQL column is applying a stricter standard than the one they wrote, and the supplier will reject the sample plan as wrong.
Inspection levels and when to move off the default
The inspection level controls how much of the lot gets looked at. ISO 2859-1 defines three general levels and four special levels, and the general default for consumer goods is Level II, used for the large majority of product inspections worldwide. The general rule stated in the reference material is straightforward: unless there is a specific reason to choose otherwise, use Level II.
Moving down to Level I makes sense when the cost of inspection is high, when the test is destructive, or when the supplier has a proven quality record and the product carries low risk. Moving up to Level III makes sense when the maximum discrimination is needed, for example on safety-critical products or with a supplier that has a history of quality problems. The four special levels S-1 to S-4 exist for destructive or extremely expensive testing where the piece is consumed, and they accept a lower level of statistical confidence in exchange for a much smaller sample.
For metal souvenirs there is a practical reason to consider Level III that has nothing to do with safety: a batch of plated parts is very hard to judge on appearance from a small sample. If the plating drift you are worried about is a bath-level change rather than a random defect, sampling will not find it because every piece in the batch drifted together. Sampling detects random defects well and systematic defects not at all. The way to catch a systematic drift is not a bigger sample but a reference: a signed plated sample held by the buyer, against which the inspector judges each piece in the sample. Our article on controlo de qualidade para presentes personalizados em metal sets out the individual checks that belong in the inspection and how to turn them into a written standard.
Switching rules: what happens across several lots
The standard does more than provide a table for one lot. It defines how the inspection regime changes over time based on results, and this is where a buyer gains real leverage in a relationship with a supplier making regular shipments.
Normal inspection is the starting point. If results indicate that quality has deteriorated, the standard recommends switching to tightened inspection, which applies a smaller sample size and stricter acceptance numbers, or discontinuing acceptance sampling altogether. If quality improves and remains stable, reduced inspection can be adopted to lower cost. The 2026 edition adds skip-lot inspection as a fourth regime, with formal procedures for switching into it from normal or reduced inspection, qualification conditions for producers and products, and validity guidance covering how batches are selected at random.
For a buyer this creates a genuine commercial incentive structure. A supplier whose lots pass consistently earns reduced inspection, which saves inspection cost. A supplier whose lots fail earns tightened inspection, which costs more and finds more. A buyer who wants to move a supplier onto skip-lot needs to satisfy the qualification conditions, and those conditions are written down in the standard rather than negotiated case by case. ISO/IEC 17025 is worth reading alongside this, because it is the standard that governs testing and calibration laboratories, and it is the reference an inspector’s competence will be measured against if a dispute goes to formal resolution.
The misconception that causes the disputes
The single most common misunderstanding is the belief that an AQL of 2.5 means the buyer accepts 2.5% defective pieces. It does not. AQL 2.5 means that a lot whose true defect rate is 2.5% will be accepted approximately 95% of the time by the sampling plan. Batches with higher defect rates face a progressively higher chance of rejection. It is a probability attached to a batch decision, not a cap on the defect rate of any individual accepted lot.
The second misconception is that AQL is a quality target. It is not. The consumer’s risk is protected by the lot tolerance percent defective, the poor quality level that the plan rejects with high probability, conventionally about 90%. Between the AQL and that limit sits the indifference quality level, where the lot has an even chance either way. A buyer who wants a quality target sets a tight AQL and accepts the cost of large samples; a buyer who wants a commercial protection sets a looser one and understands the sampling risk that comes with it.
The third misconception is that AQL 2.5 is a universal number. It is the most widely used default, and the reference material describes it as the most common setup in international trade for critical, major and minor defects at General Level II. But a promotional giveaway and a precision component do not belong in the same plan, and the framework exists precisely so the level can be calibrated to the risk.
Writing the acceptance clause
Everything above becomes usable when it is written into the purchase order in a form an inspector can apply without phoning anyone. A workable clause names, in order: the standard and edition being applied; the lot definition, including whether split lots by colour, size or plating are treated separately; the inspection level; the AQL for each defect class, with the classification written against physical features; the sample size and accept and reject numbers resulting from the lookup, so there is no interpretation left; the reference standard the inspector uses for colour and finish; the inspection timing and condition, including lighting and whether parts are presented packed or unpacked; and the disposition rules for a failed lot.
Two clauses need particular care in this category. The first is the colour and finish reference. An inspector arriving with no reference is judging against their own memory, and two inspectors will not agree. Attach the signed plated sample, describe the reference in writing, and if a physical standard is impractical, define the band numerically and name the measurement method and instrument.

The second is the disposition of a failed lot. The standard defines acceptance and rejection; it does not define what happens next. A buyer who has not specified this faces three possible outcomes at the moment of failure: the lot is rejected and the supplier sorts or replaces it, the lot is accepted against a concession, or the lot is re-inspected under tightened inspection with a new sample. This extended AQL reference covers the switching behaviour and the AQL range from 0.065 for critical defects to 6.5 for cosmetic-only issues, which is the range most often needed when one order contains both a functional accessory and a purely decorative item.
One timing point is specific to metal souvenirs and worth including explicitly. If the lot contains parts with tight dimensional tolerances, the inspection cannot be performed on parts that have not completed ageing, because measuring an un-aged casting to a tight tolerance produces a false accept that will subsequently move out of tolerance in service. Either the parts are aged before the inspection, or the inspection measures characteristics that ageing does not affect. This is not a dispute mechanism, it is a physics constraint, and it is better stated in advance.
A worked acceptance example
The following shows the complete chain for a specific order, which is the format most useful for a buyer who wants to write their own clause. The order is 3,000 custom zinc alloy souvenir pieces, General Inspection Level II, with defect classes critical at 0, major at 2.5 and minor at 4.0.
| Step | Input | Result |
|---|---|---|
| Lot definition | 3,000 pieces, one colour, one plating, one size | Single lot, not split |
| Inspection level | General Level II | Table 1 lookup required |
| Table 1: code letter | Lot 1,201 to 3,200 at Level II | Code letter K |
| Table 2: sample size | Code letter K | 125 pieces drawn at random |
| Critical, AQL 0 | Accept 0, reject 1 | One critical defect fails the lot |
| Major, AQL 2.5 | Accept 14, reject 15 | Lot fails at 15 major defects |
| Minor, AQL 4.0 | Accept 21, reject 22 | Lot fails at 22 minor defects |
| Outcome | All three classes must pass | Single sampling, one decision per lot |
The same chain applied to a smaller order shows why the lot size matters less than buyers expect. An order of 500 pieces returns code letter H and a sample of 50, so the lot is accepted on 3 major defects and rejected on 4 — a much tighter absolute margin than the 3,000-piece order, which is accepted on 14 and rejected on 15. Small lots are inspected more strictly in absolute terms because the sample size is a large fraction of the lot, and the accept and reject numbers have nowhere to go. A buyer who finds this counter-intuitive should check the plan against a written table before the shipment rather than after the dispute.
Two commercial notes close this out. Inspection cost scales with sample size, so the level choice is a cost decision as much as a quality decision: Level II on a 12,000-piece order means 315 pieces examined, while the same order at Level I means a smaller sample. And a supplier that has passed repeatedly can be moved to reduced or skip-lot inspection under the rules of the 2026 edition, which lowers the cost of goods for both parties. For the lead time side of the same order, our guide to how much custom metal gifts cost sets out how inspection scope and order quantity interact on the unit price, and our article on custom metal gifts MOQ explains the three minimum order quantity tiers that determine whether a design gets its own mould.
Before the inspection clause is drafted, the drawing has to exist, because dimensional acceptance has nothing to refer to otherwise. The production stages that produce that drawing are covered in our guide to going from a 3D model to a metal souvenir, including where tolerance indications belong in the document set.
Send your order specification and your defect classification to sales@kingtopgift.com, and ask for the resulting sample size and accept and reject numbers before the first batch runs. That table is short, and it is the cheapest insurance in the whole transaction.